An impressive project
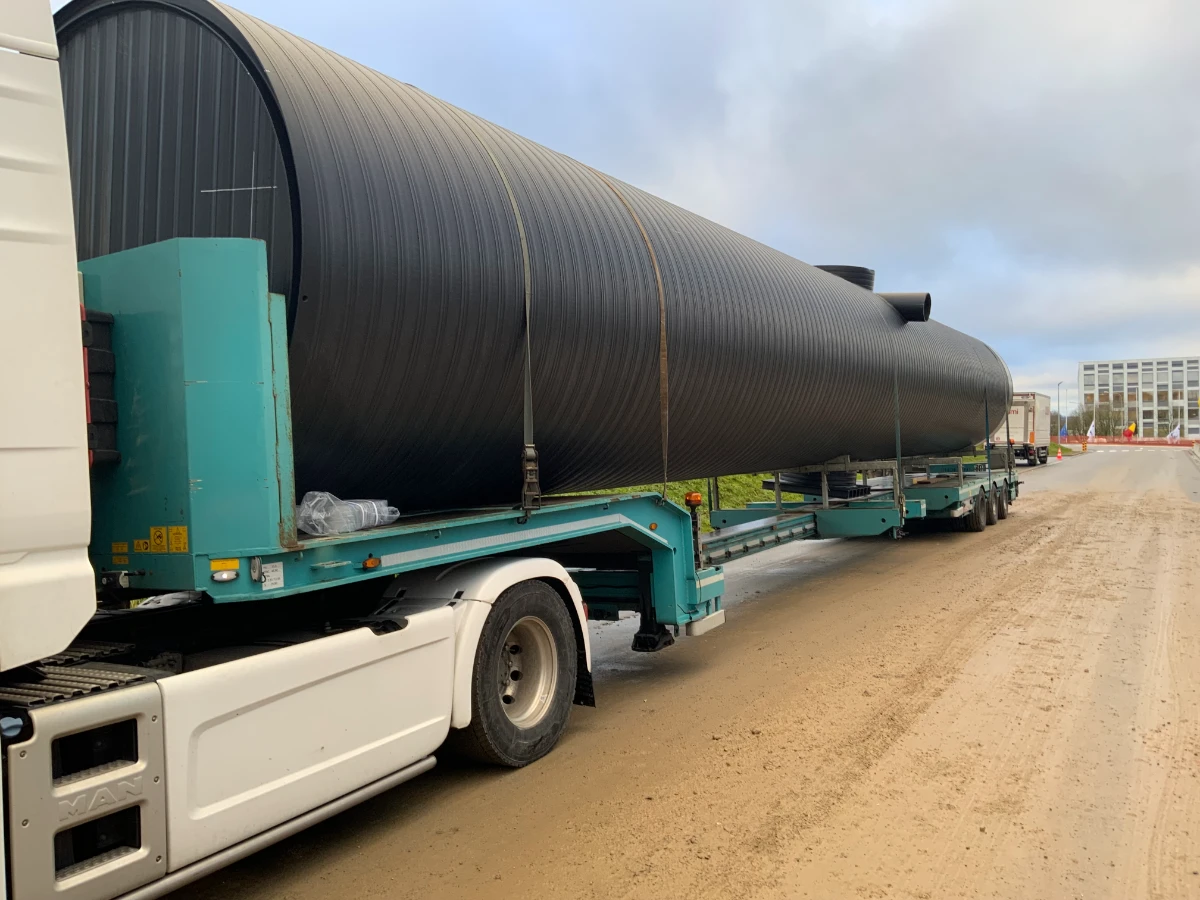
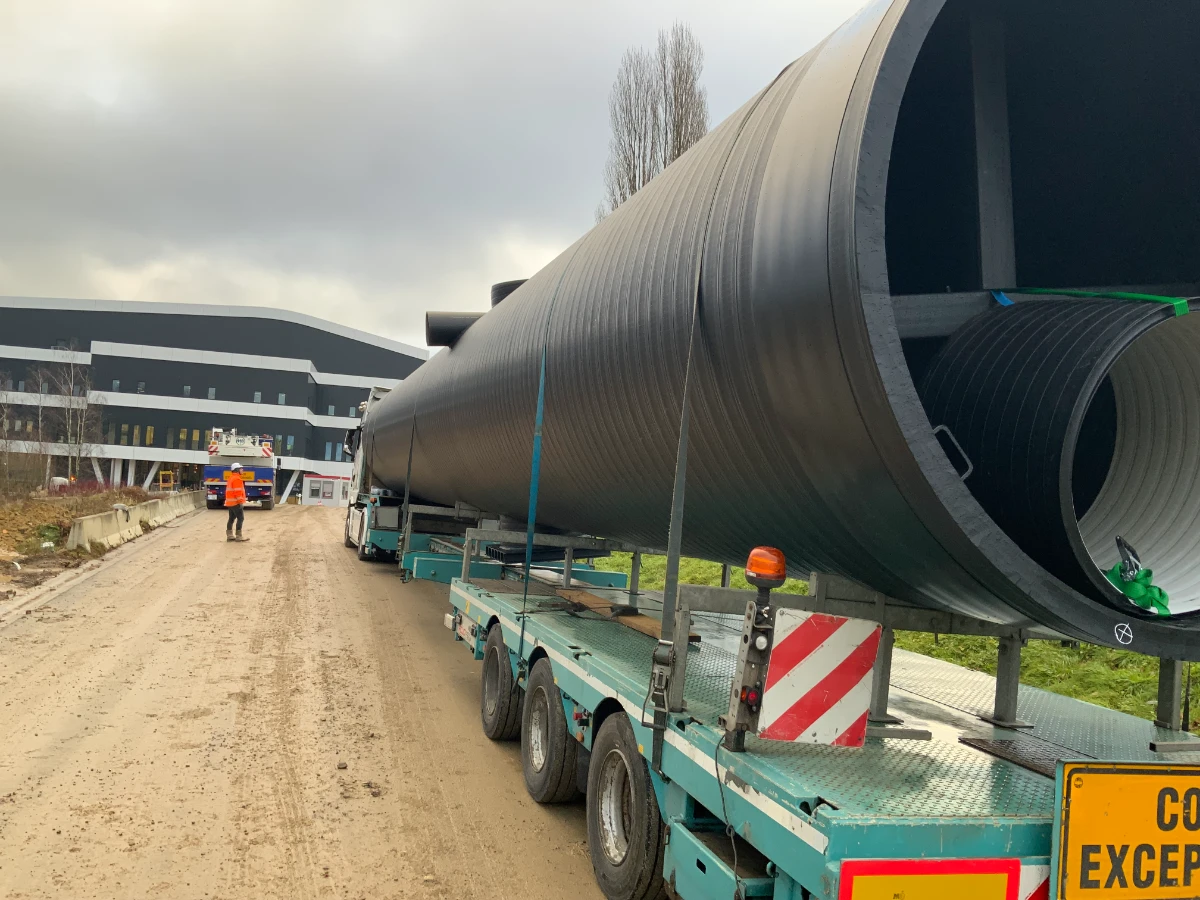
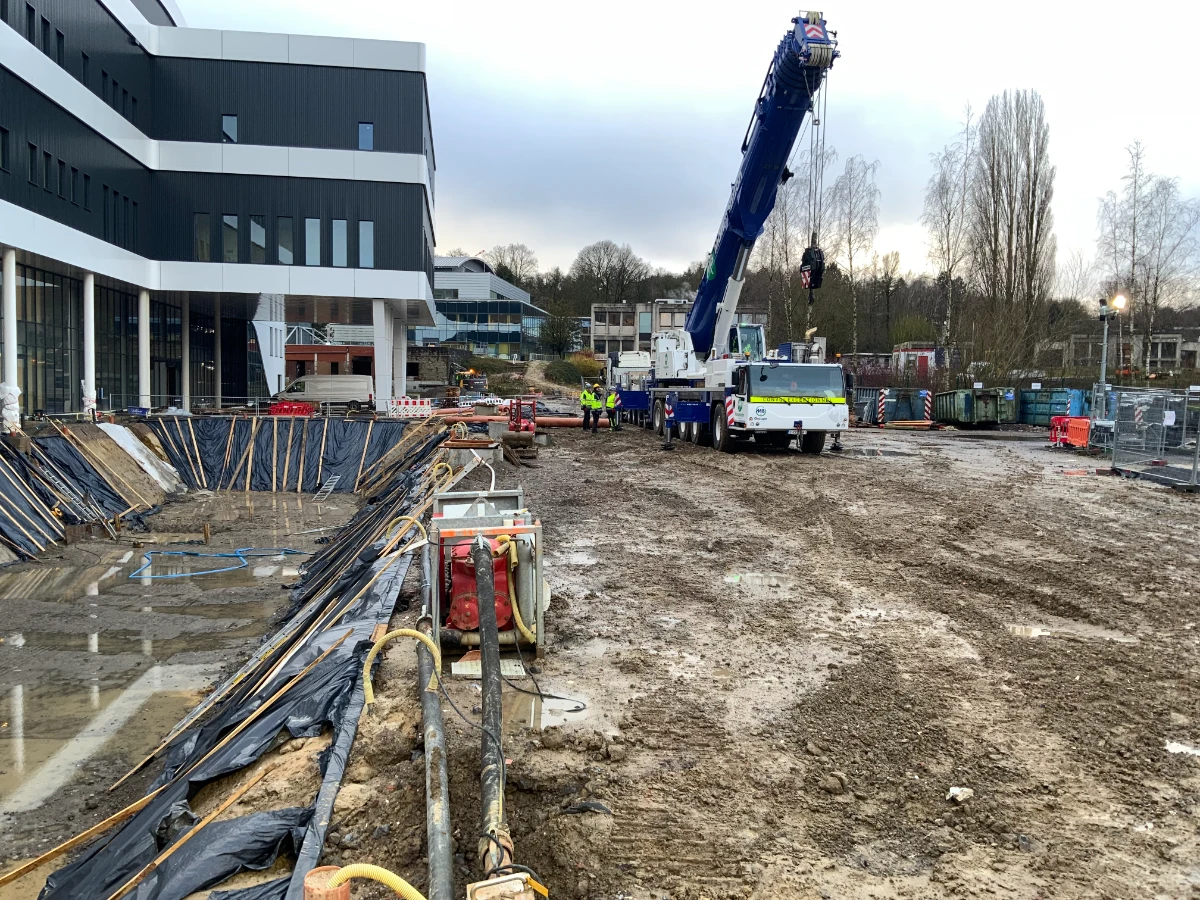
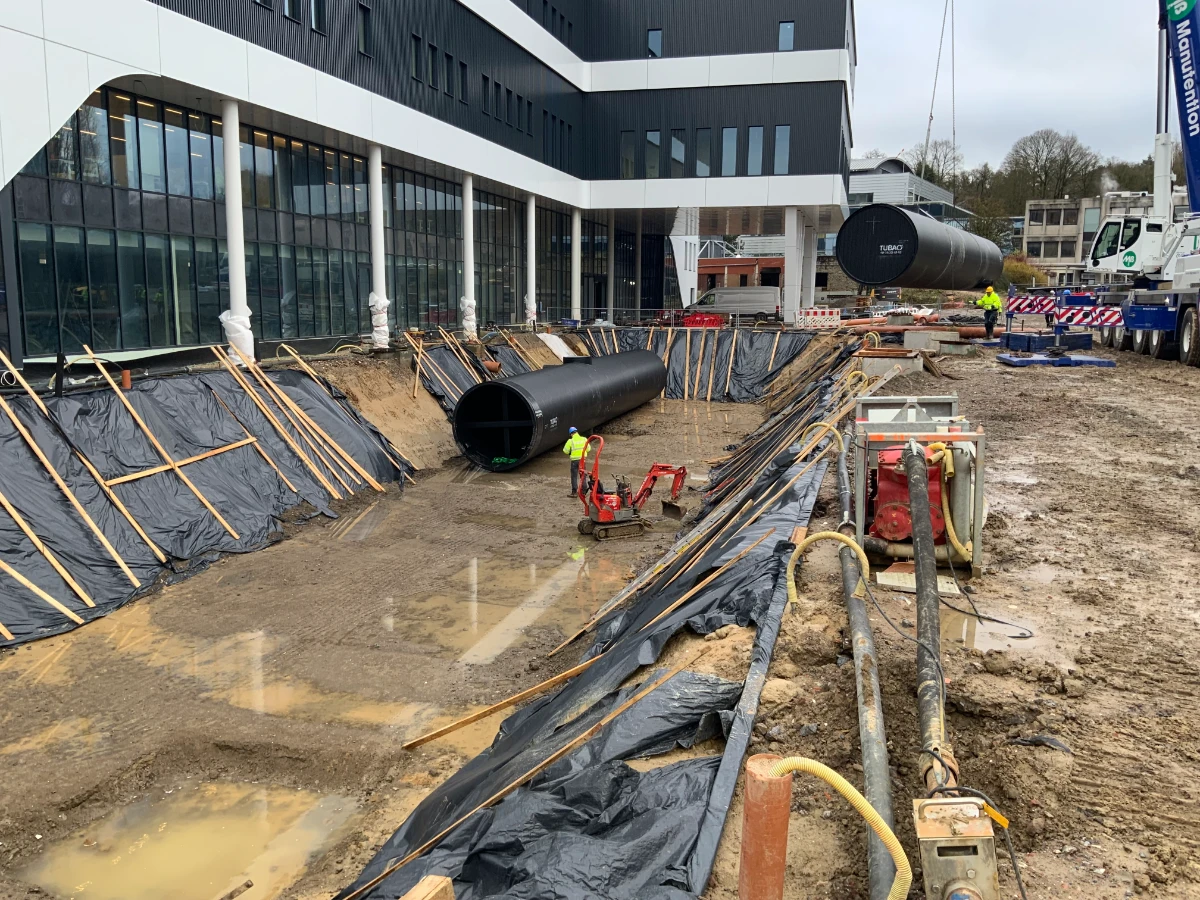
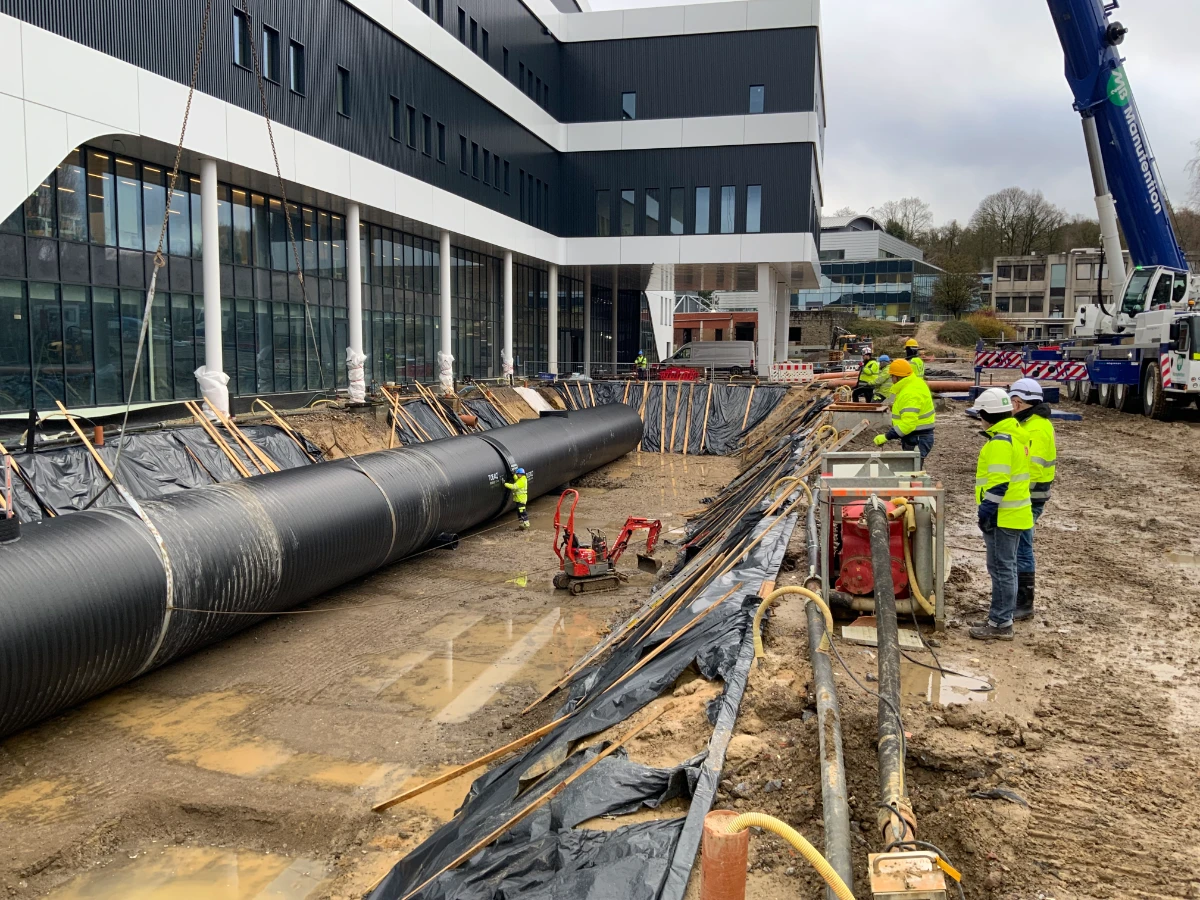
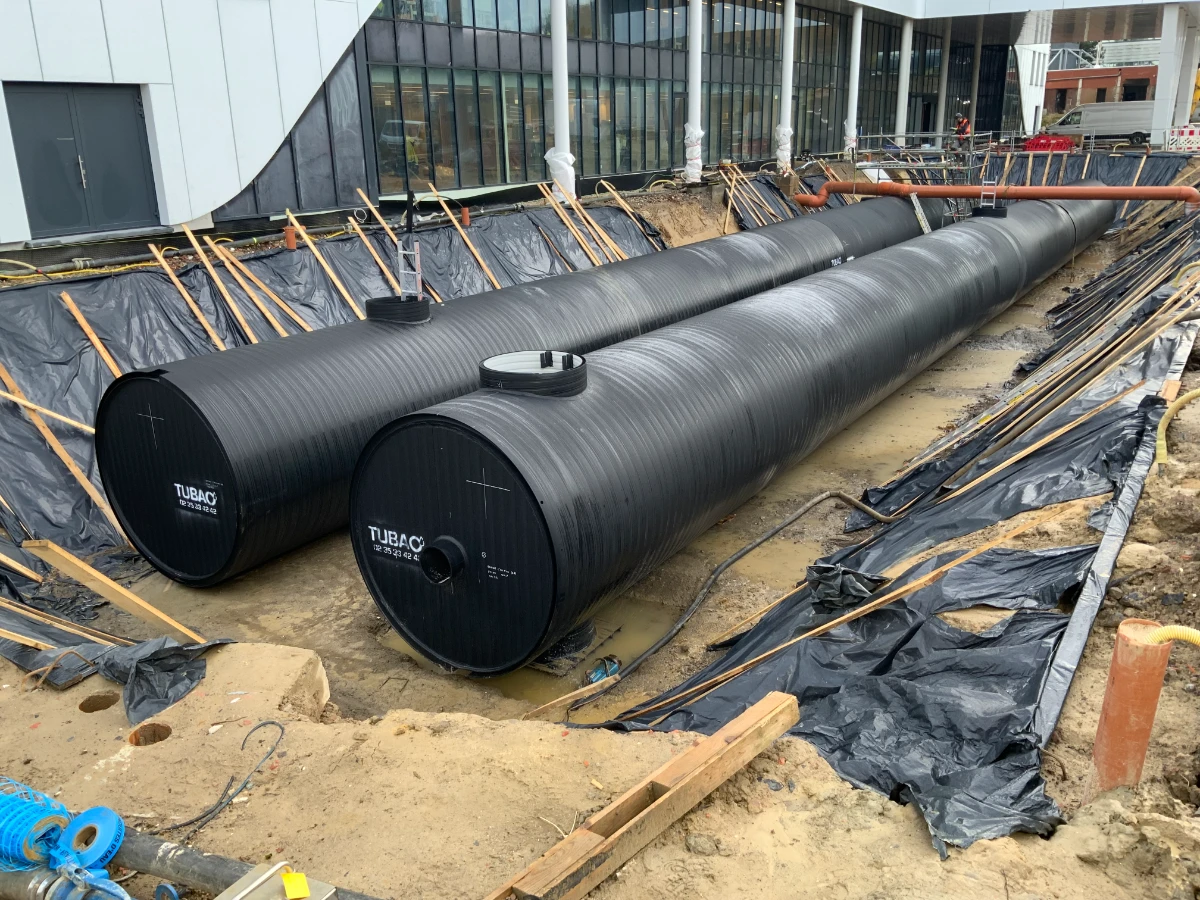
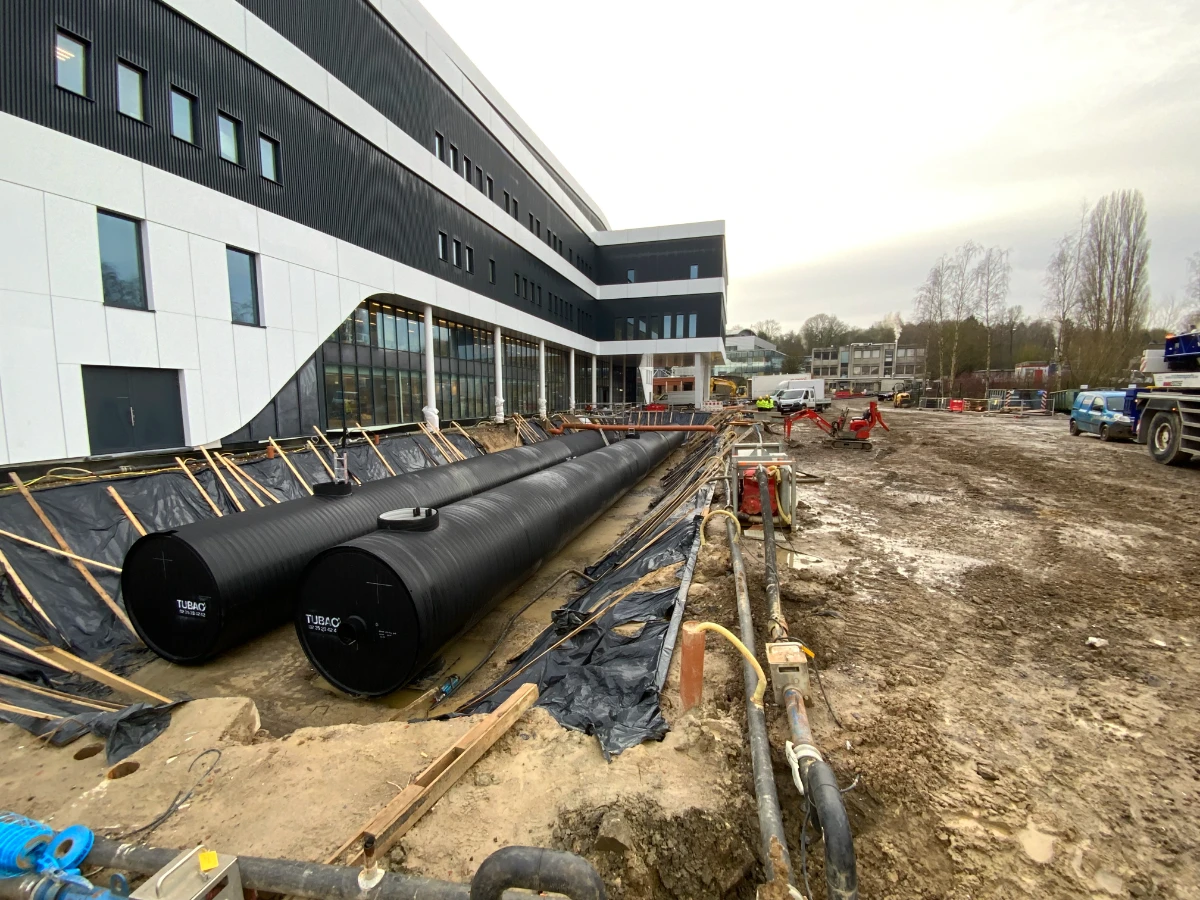
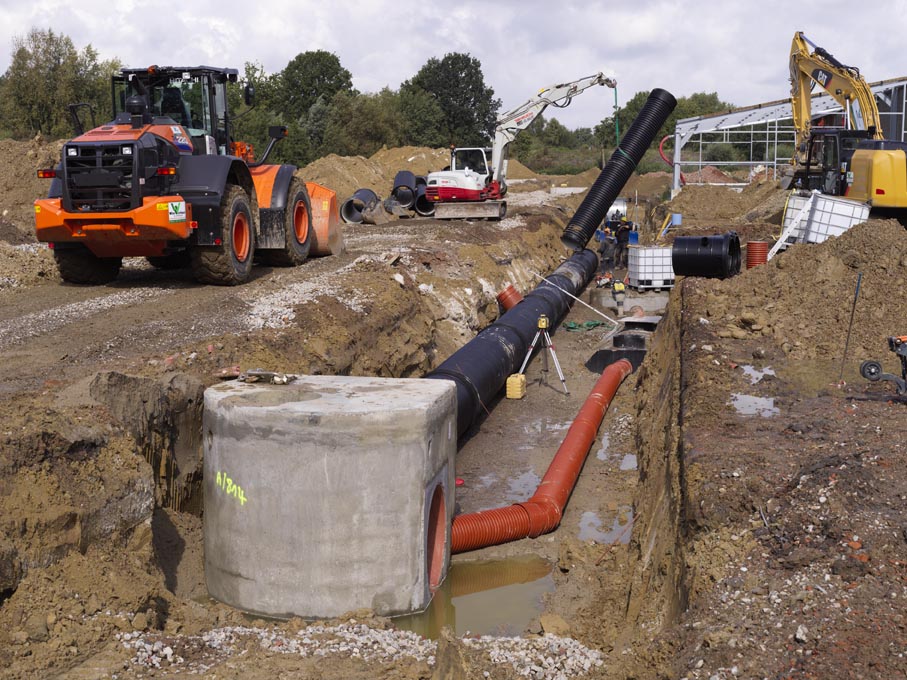
The pharmaceutical company UCB recently had a new building constructed at its site in Braine-l'Alleud, which required efficient rainwater management. In collaboration with contractor Wanty, architectural firm Syntaxe, and the engineering department of sister company Collinet, an advanced technological solution was implemented: an underground reservoir with a storage capacity of no less than 360 m³ of rainwater. This was made possible by the installation of four custom-made underground HDPE Weholite storage tanks produced by Collinet.
A new building dedicated to innovation and manufacturing
The project involves the construction of a new building called “Genesis”, which focuses on research & development and the installation of a new pharmaceutical production facility. Architectural firm Syntaxe called upon Collinet and Tubao to find a solution for the development of a storage and buffer tank, which was originally planned in concrete. After several discussions with the architect and UCB, it appeared that the Weholite HDPE tanks were the most suitable solution. The final technical adjustments were carried out in collaboration with the company Wanty.
Technical expertise and innovation of Collinet
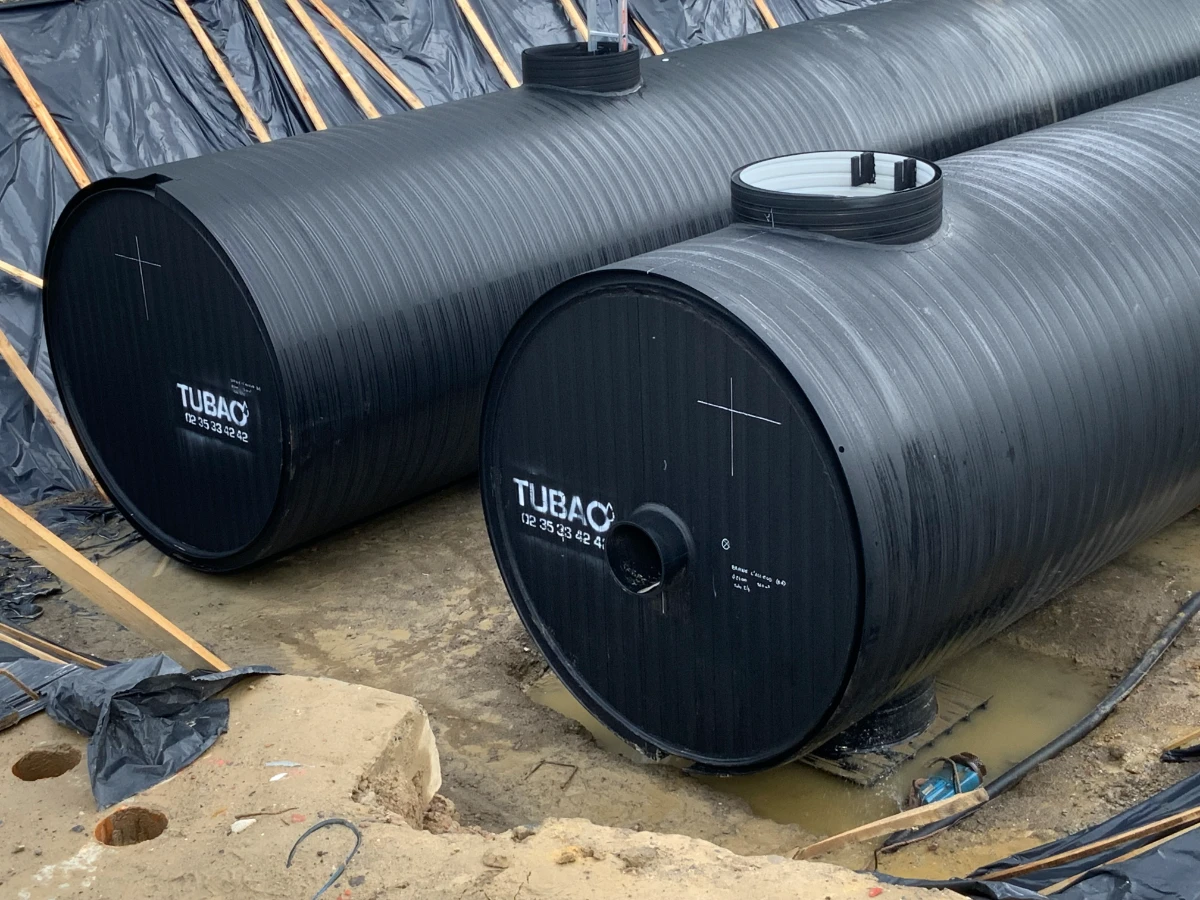
Collinet, a specialist in sustainable HDPE solutions, designed and manufactured these retention basins specifically for this project. The double-walled Weholite HDPE tanks, manufactured in France by exclusive partner Tubao, are distinguished by their innovative design, which ensures perfect watertightness and exceptional durability.
Fast and efficient installation
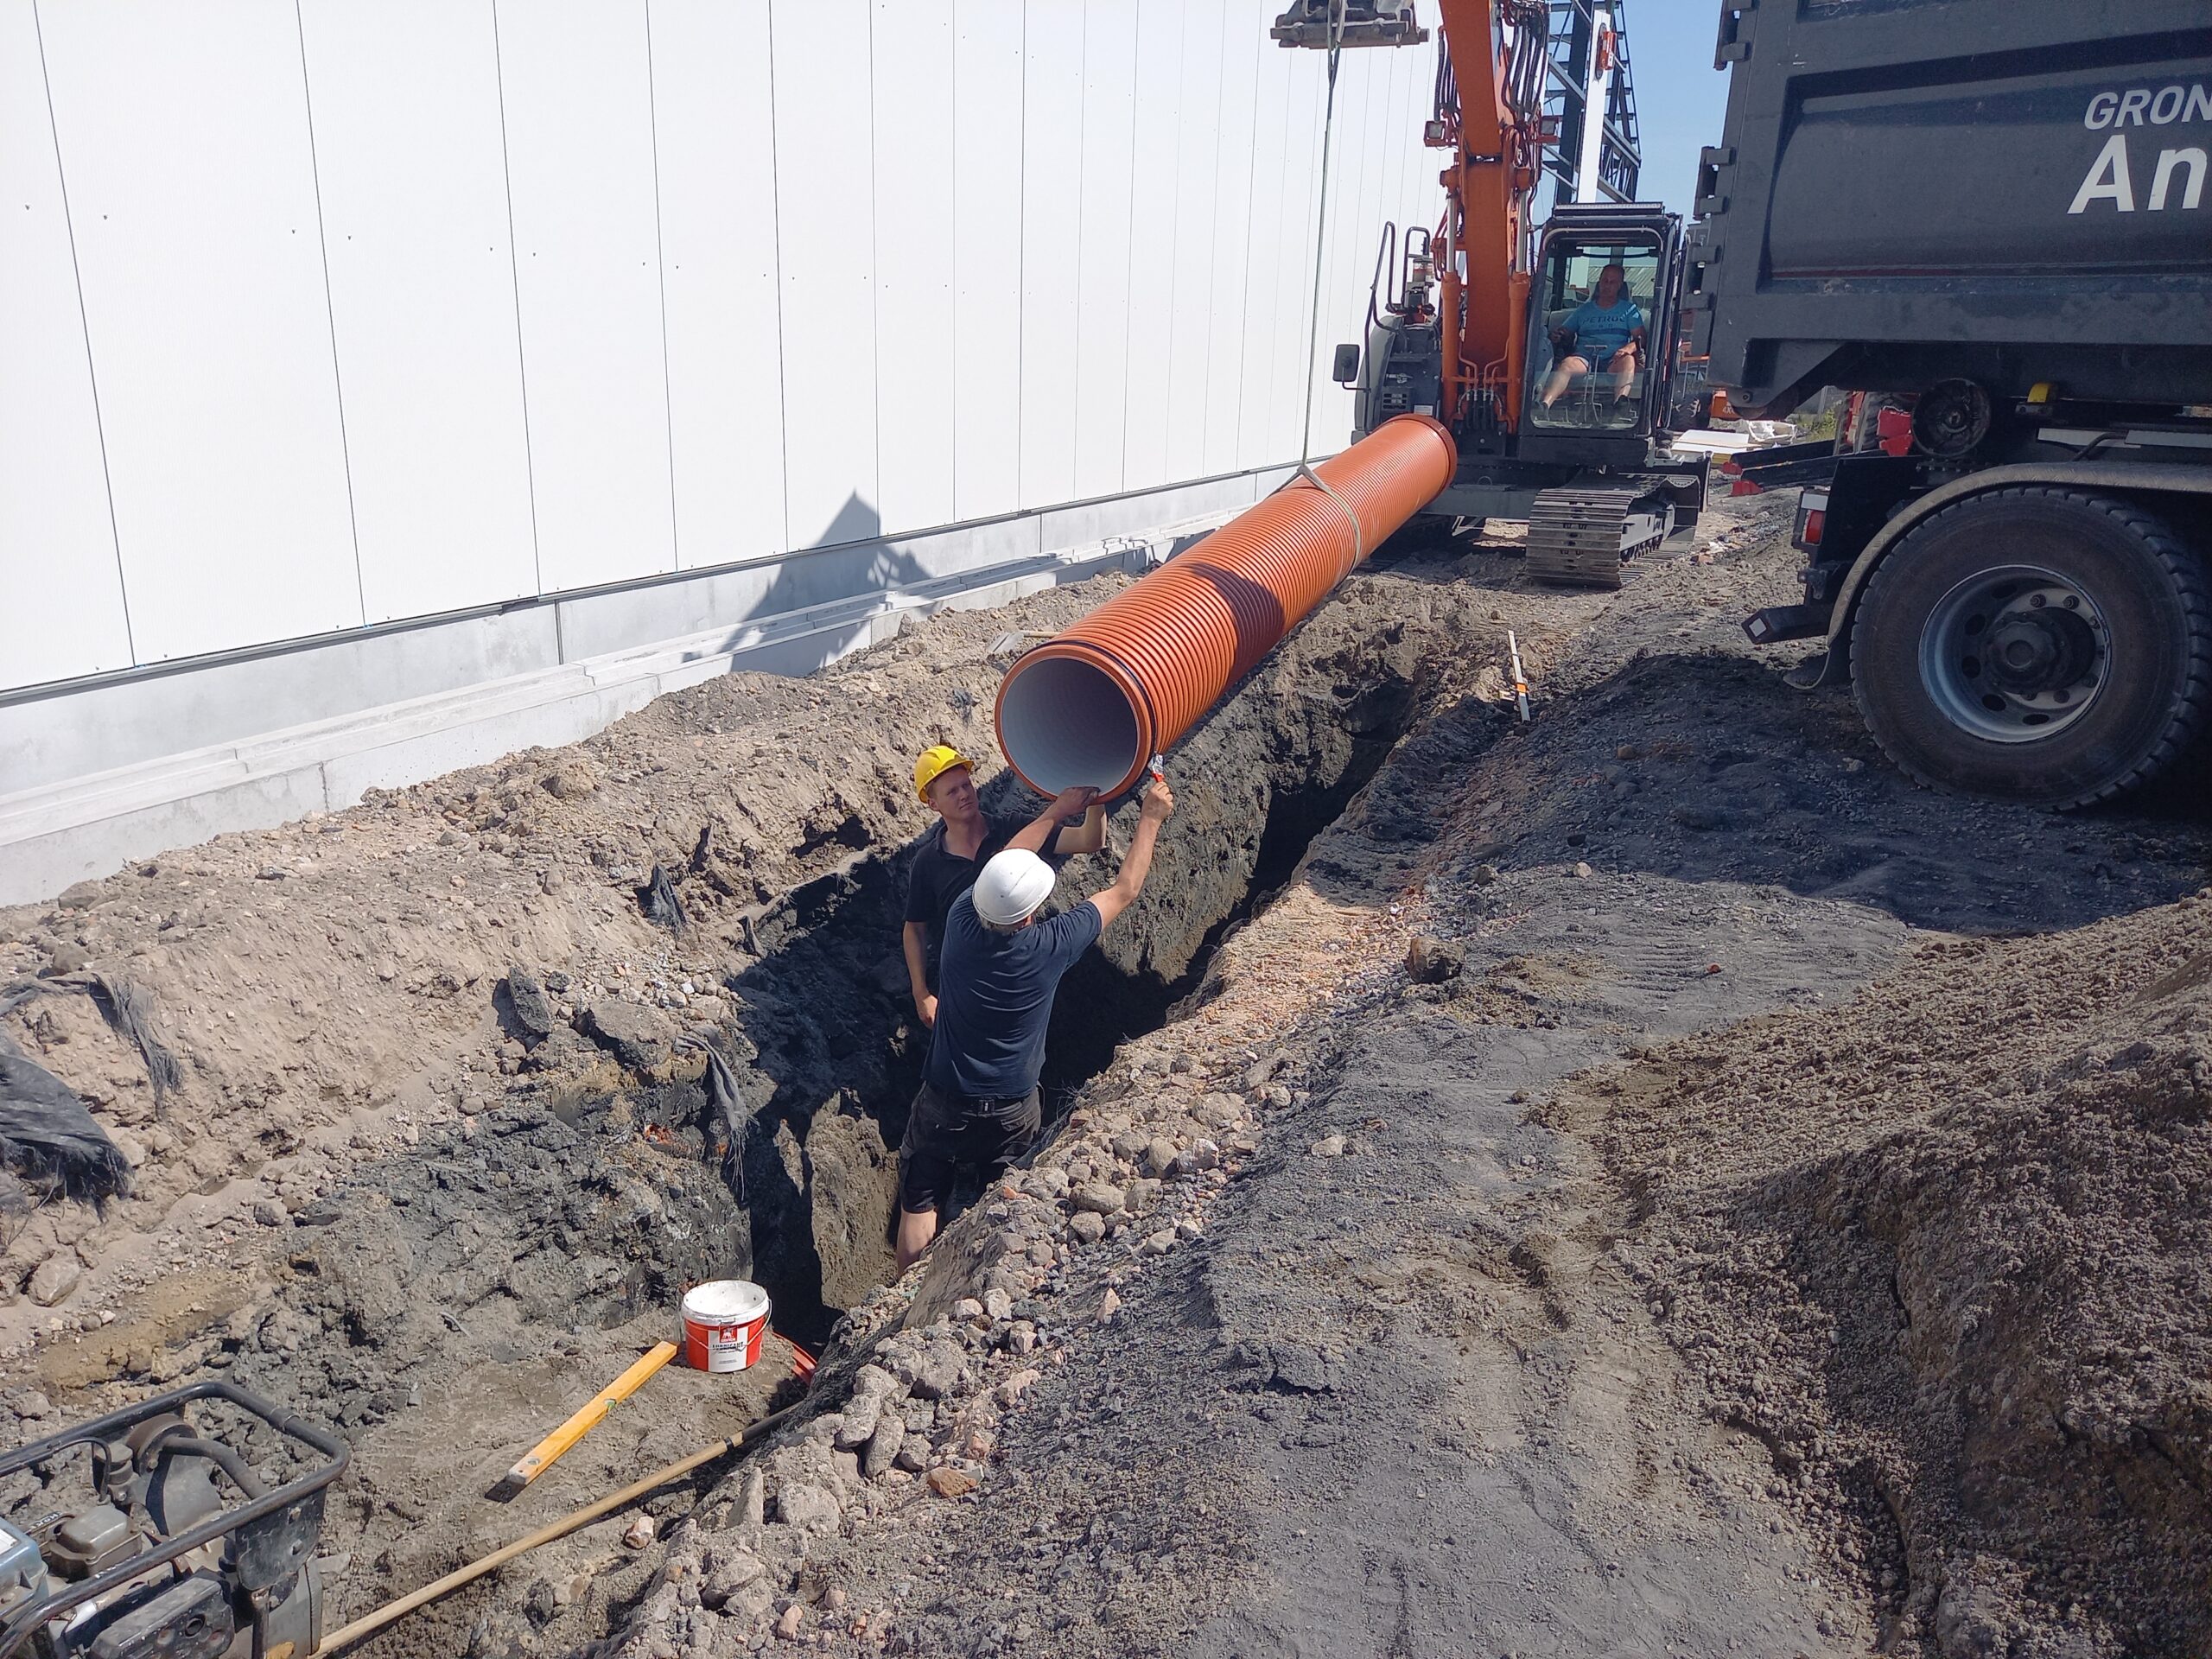
What makes this project even more remarkable is the installation of the four tanks, each 20 meters long. Their placement on the site took only two days – an exceptionally short execution time for a project of this scale. This testifies to Collinet's technical precision and careful preparation.
Optimizations for a perfect fit
Dimitri Steilen, head of the Wallonia design office, led this ambitious project and anticipated all necessary adaptations to meet the site requirements. He explains:
“The permit for this project required a buffer volume of 300 m³, to which we added another 60 m³ to collect and reuse rainwater. This optimization was made possible thanks to the installation of an HDPE partition wall in one of the tanks.”
Collinet also contributed to the installation of the booster pumps, in cooperation with partner Ecosolutions, which were integrated directly into the Weholite structure.
“An important point of attention was the presence of groundwater,”
adds Dimitri. Because the tanks were largely placed below the groundwater level, a buoyancy study was carried out by manufacturer Tubao. This study showed that the construction was stable, making an additional anchoring system unnecessary.
Why choose HDPE?
The choice of HDPE was strategic: this material is known for its robustness and exceptional longevity. It offers increased resistance to the most demanding conditions and guarantees optimal long-term performance. Moreover, the double-walled structure contributes to extra safety and structural integrity.
An industry first
This site marks a first: buffer tanks of this size made of HDPE have never been installed on site before. Thanks to Collinet's technical expertise, the contractor was completely unburdened. The on-site connections were prepared to perfection, which guaranteed a smooth and efficient installation.
A sustainable solution for rainwater management
Buffer basins such as this play a crucial role in the storage and reuse of rainwater. This project demonstrates how innovative materials and custom-made solutions contribute to sustainable water management in industrial applications. With this successful completion, Collinet once again confirms its expertise in the design and production of high-tech HDPE solutions for water storage and treatment.
Why choose the double-walled Weholite HDPE storage tanks from Collinet?
Our tanks offer unprecedented benefits for industrial storage:
- Full VLAREM II compliance: Collinet is the only manufacturer that offers underground VLAREM II-approved tanks.
- Durable and leak-proof construction: made of Weholite HDPE, completely corrosion-resistant.
- Space-saving: underground installation prevents the loss of usable space and integrates seamlessly into industrial drainage systems.
- Maximum safety: equipped with advanced detection and security systems.
- Custom-made solutions: tanks are tailored to the specific needs of your project.